

Recent Posts
 What does an oral liquid cap puncture force tester measure?Sep 16, 2026
 How puncture force testing helps control oral liquid cap consistencySep 16, 2026
 Rubber Stopper Puncture Force Testing for Reliable Vial Closure Quality ControlSep 15, 2026
 Building an ASTM-Aligned Plastic Film Puncture Test Method for Incoming QCSep 15, 2026
 7 Critical Parameters to Evaluate When Selecting a Syringe Needle Tester for ISO 7886 ComplianceSep 14, 2026
How Puncture Force Testing Helps Control Oral Liquid Cap Consistency
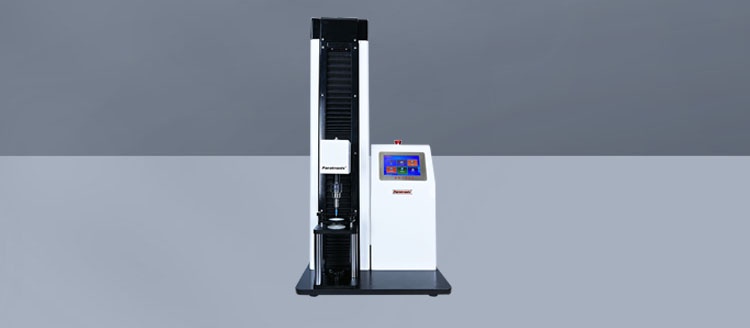
Consistent cap performance is essential for protecting oral liquid products, maintaining user safety, and reducing packaging-related risk. An oral liquid caps puncture force Tester provides objective data to verify opening resistance, material uniformity, and sealing reliability across production batches. For pharmaceutical packaging decision-makers, puncture force testing supports tighter quality control, faster issue detection, and more confident compliance with demanding packaging standards.
The issue is often more complex than it first appears. A cap may look identical from one delivery lot to the next, pass a visual inspection, and still behave differently when a patient, caregiver, dispensing device, or production-line needle interacts with it. A slightly thicker pierceable zone, an uneven wall profile, a material formulation change, or a shift in molding conditions can alter the force needed to penetrate the cap. That change may not be visible, but it can affect usability, leakage risk, or compatibility with downstream equipment.
For companies responsible for pharmaceutical packaging, the goal is not simply to obtain a single force value. The real objective is to establish whether cap performance remains stable, predictable, and appropriate for the intended use throughout the supply chain and product lifecycle.
Why cap consistency deserves direct measurement
Oral liquid closures can serve several functions at once. They may protect the formulation from contamination, maintain the integrity of a primary container, provide evidence of opening, support controlled dispensing, or accommodate a piercing action during filling, sampling, reconstitution, or use. In these applications, the cap is not merely a decorative closure. It is a functional component whose mechanical response matters.
A puncture force result reflects the resistance encountered as a probe penetrates a defined area of the cap under controlled conditions. When the test setup is held constant, variations in the force curve can reveal changes in the cap itself. These may include differences in polymer grade, elastomer hardness, thickness distribution, laminate structure, mold wear, curing behavior, internal stress, or storage history.
Without a controlled mechanical test, manufacturers often rely on indirect signs: complaints from filling operations, intermittent needle damage, inconsistent opening feedback, unusual leakage findings, or operator observations. Those signals matter, but they arrive late and are difficult to quantify. Puncture force testing turns a subjective concern into data that quality, procurement, engineering, and suppliers can discuss using the same reference point.
This does not mean that puncture force alone proves package suitability. A cap can meet a force target and still require evaluation for torque, seal integrity, dimensional fit, chemical compatibility, transport performance, or child-resistant function where applicable. It is, however, a practical way to control one of the failure modes that visual checks and basic dimensional inspection may miss.
What the force curve can reveal
A well-designed test does more than report a peak load. The shape of the force-versus-displacement curve can help teams distinguish between different types of inconsistency. Rising resistance before penetration, a sharp maximum at breakthrough, post-puncture behavior, and the consistency of repeated profiles may each provide useful context.
For example, a higher-than-usual peak puncture force may point to increased material thickness, reduced elasticity, a tougher resin blend, or a change in the intended puncture location. A lower force may indicate thinner material, insufficient structural strength, a defect in the membrane area, or material degradation. Neither outcome should automatically be called good or bad. The acceptable direction depends on how the closure is used and on the product’s validated packaging requirements.
Variability is often as informative as the average. A batch with a reasonable mean value but wide scatter can create sporadic line interruptions or uneven user experience. In practice, a production line rarely experiences “the average cap.” It encounters individual caps. Looking at the spread of results, the location of outliers, and repeatability between test positions gives a more realistic view of operational risk.
Test conditions define whether results are meaningful
Comparing force data is only useful when the test method is stable. Probe geometry, probe tip condition, penetration speed, test direction, penetration depth, cap support method, sample conditioning, and puncture location can all influence the result. A blunt probe and a sharp probe will not produce interchangeable data. Nor will a test performed on an unsupported cap necessarily represent the behavior of a cap assembled on its bottle or seated in its actual closure system.
This is why an oral liquid caps puncture force Tester should be selected as part of a method-development exercise rather than treated as a generic force gauge. The fixture must prevent shifting or deformation that is unrelated to the puncture event. The selected probe should represent the actual functional interaction as closely as possible. If the production process uses a specific needle, cannula, or piercing element, its relevant dimensions and geometry should inform the testing approach.
Environmental controls also deserve attention. Some polymers and elastomeric materials respond differently after exposure to temperature or humidity changes. If samples are conditioned differently before test, apparent lot-to-lot variation may be caused by handling rather than manufacturing. The testing procedure should therefore specify storage conditions, equilibration time, sampling locations, and the number of units evaluated. The appropriate details depend on the package design and internal quality plan.
Where puncture force testing fits in quality control
The most effective programs use puncture testing at points where it can answer a decision-making question. For incoming inspection, it can help verify that a supplied closure lot performs within an agreed operating range before it enters production. During process validation or package development, it can be used to compare materials, cap designs, molding settings, or supplier samples. During routine production, it may serve as a trend-monitoring tool when cap function is particularly sensitive.
It is also valuable during investigations. When a filling line reports inconsistent piercing, teams often begin by reviewing equipment condition and operating settings, which is sensible. Yet the closure lot should not be assumed innocent. Retained samples tested under the same method can help separate a cap-related shift from a machine-related issue. That distinction can prevent lengthy troubleshooting based on incomplete evidence.
A common mistake is setting an acceptance limit before understanding normal process behavior. If historical data are limited, it is usually wiser to establish a controlled baseline with representative samples, then define appropriate limits through the company’s quality and risk-management process. Limits should be connected to functional requirements, not copied from an unrelated package format.
Choosing the right testing approach
Decision-makers evaluating a puncture force system should look beyond the advertised force range. The key question is whether the instrument can reproduce the real application with sufficient control and traceability. A system should support the relevant probe, fixture, travel path, speed, data capture, and reporting needs for the closure under evaluation.
For oral liquid caps, the fixture is frequently the difference between useful data and misleading data. A closure that flexes, rotates, or is clamped too aggressively may generate a result that reflects the fixture more than the material. Where the cap is normally tested in an assembled condition, a fixture designed around the bottle-cap combination may be more appropriate than a flat-sheet arrangement. Where testing focuses on a dedicated pierceable region, positioning repeatability becomes especially important.
Software and data handling should fit the quality workflow as well. Teams may need to retain full force-displacement curves, identify peak force automatically, export raw results, compare lots, or review trends over time. The exact documentation and electronic-record expectations depend on the organization’s procedures and regulatory environment, but these requirements should be clarified before equipment selection rather than after installation.
Paratronix Instruments Co., Ltd. develops packaging testing instruments for pharmaceutical packaging, plastic packaging materials, high-barrier materials, and related applications. In a puncture-force project, the useful contribution is not simply supplying a tester. It is helping define the test configuration around the package: what is being punctured, where it is punctured, how the sample is held, which data point governs the decision, and how the method can be repeated by different operators.
Turning test data into practical control
Once a method is established, the value comes from disciplined use. Results should be reviewed by lot, supplier, mold cavity where traceability permits, production date, and material or process change. A gradual shift can be more significant than one isolated result, particularly where it approaches a level that could affect automated piercing or intended user interaction.
When an outlier appears, the first response should not be to adjust the acceptance criteria. Confirm the sample orientation, probe condition, fixture setup, and conditioning history. Then compare retained samples and related packaging checks. If the shift remains, the investigation can move toward cap manufacturing variables, raw material records, storage exposure, or assembly conditions. This sequence keeps the test from becoming a standalone number with no operational context.
Puncture force testing is most useful when it is tied to a specific risk: a cap that must be pierced reliably, a membrane whose thickness must remain controlled, or a closure lot that may affect filling-line performance. For these situations, objective mechanical measurement provides an early warning that visual inspection cannot provide. The right oral liquid caps puncture force Tester, paired with a representative fixture and a controlled method, gives packaging teams a clearer basis for approving lots, investigating deviations, and maintaining consistency as materials and suppliers evolve.
Before finalizing a testing solution, confirm the cap construction, intended puncture mechanism, sample condition, expected throughput, reporting needs, and any internal or market-specific requirements. Those details determine whether a force measurement becomes a dependable quality-control tool or merely another number in a report.
Leave A Reply
Search by Keywords