

Recent Posts
 7 Critical Parameters to Evaluate When Selecting a Syringe Needle Tester for ISO 7886 ComplianceSep 14, 2026
 Can an infrared method water vapor permeability tester replace gravimetric testing for ISO 15106-3 compliance?Sep 14, 2026
 Comparing Gravimetric, Coulometric, and Modulated IR WVTR TestersSep 11, 2026
 Choosing the Right Water Vapor Transmission Rate Tester: Pharmaceutical Packaging LabsSep 11, 2026
 Which ASTM Methods Apply to Sauce Packet Pressure Resistance Burst and Creep Tests?Sep 08, 2026
7 Critical Parameters to Evaluate When Selecting a Syringe Needle Tester for ISO 7886 Compliance
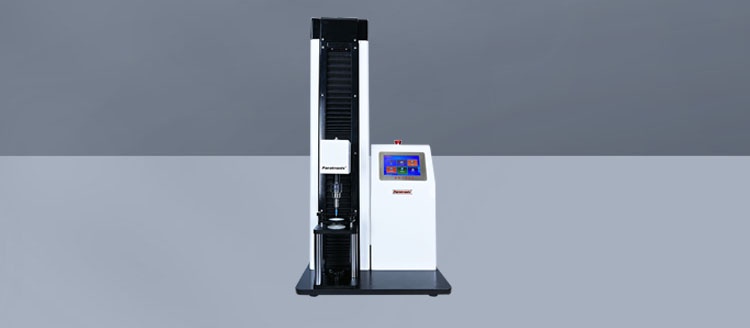
Ensuring syringe needle safety and performance is non-negotiable for pharmaceutical quality control and regulatory compliance. A reliable syringe needle tester is essential to verify needle strength, sharpness, and resistance to bending or breakage per ISO 7886 standards. For QC and safety professionals, selecting the right tester means balancing precision, repeatability, traceability, and ease of integration into existing lab workflows. This guide outlines 7 critical parameters—ranging from force measurement accuracy and fixture compatibility to software validation and audit readiness—that directly impact test validity and regulatory acceptance.
1. Force Measurement Accuracy—and What “±0.5%” Really Means in Practice
ISO 7886-1:2017 specifies force tolerances for needle penetration, deflection, and break tests—often down to ±0.25 N for 1.0 N nominal loads. But quoting “±0.5% full scale” on a spec sheet doesn’t tell you whether that uncertainty holds across the entire working range (e.g., 0.1–10 N), at low-force thresholds where needle tip deformation begins, or after thermal drift over a 4-hour test session. Real-world calibration traceability matters more than theoretical resolution. Look for instruments with dual-range load cells calibrated to ISO/IEC 17025-accredited labs—not just factory-certified—and verify how often recalibration is recommended under routine lab conditions.
2. Fixture Design: Not Just “Standard Compliant,” But Fit-for-Purpose
A fixture that accepts ISO 7886’s defined needle diameters (0.3–1.2 mm) and hub geometries sounds sufficient—until you run 30-gauge insulin needles next to 18-gauge IV catheter needles on the same mount. Poorly designed fixtures introduce lateral play or inconsistent axial alignment, skewing deflection results by up to 12% in comparative studies. The best systems use modular, self-centering collets with adjustable clamping torque—not fixed-thread adapters—and allow quick-swapping without realignment. If your lab tests both glass- and polymer-based syringes, confirm the fixture accommodates varying hub stiffness without slippage during high-speed penetration cycles.
3. Test Speed Control: Why “Variable Rate” Isn’t Enough
ISO 7886 mandates specific test speeds: 10 mm/min for penetration, 1 mm/min for deflection, and 100 mm/min for break testing. But speed consistency isn’t just about motor specs—it’s about closed-loop feedback during load spikes. A stepper motor may claim “±1% speed accuracy,” yet overshoot when encountering sudden resistance from a hardened stainless steel needle. Servo-driven systems with real-time position/load feedback maintain ±0.3% speed tolerance even under peak load. That difference becomes decisive when comparing batches near specification limits—or when investigating root cause of premature needle fracture.
4. Data Integrity Architecture: Beyond “Export to Excel”
Regulatory auditors don’t ask if data *can* be exported—they ask how it’s protected *before* export. A compliant syringe needle tester must enforce user roles (e.g., operator vs. reviewer), embed digital signatures, log all parameter changes with timestamps, and prevent post-test editing of raw force-displacement curves. “Audit trail enabled” isn’t enough if the system allows disabling logs via local admin override. True integrity starts with hardware-enforced write-once storage for raw sensor data—and continues through encrypted database backups that meet 21 CFR Part 11 Annex 11 expectations for electronic records.
5. Environmental Stability: Temperature, Humidity, and Vibration Sensitivity
Needle stiffness varies measurably with ambient temperature—especially for polymer-coated or nitinol variants. Yet many testers assume lab conditions are stable. Units without internal temperature compensation or environmental monitoring risk ±3% deviation in yield force between 20°C and 25°C. Similarly, unisolated load cells can pick up floor vibration from nearby centrifuges or HVAC units, adding noise to low-force penetration profiles. Check whether the instrument includes passive thermal shielding, active temperature stabilization, or vibration-dampening feet—and whether those features are validated under your actual lab conditions, not just in an anechoic chamber.
6. Software Validation Support: Not Just “IQ/OQ Ready”
“Validatable software” is meaningless unless the vendor provides documented evidence—not just templates. You need pre-written URS (User Requirement Specifications), FRS (Functional Requirement Specifications), and traceable test protocols covering every function invoked during ISO 7886 testing: auto-zero routines, curve smoothing algorithms, pass/fail logic for slope detection, and report generation logic. Paratronix Instruments Co., Ltd., as a professional manufacturer of packaging testing instruments for pharmaceutical packaging, plastic packaging material, and high barrier material, structures its software documentation around these deliverables—not as add-ons, but as integral to the platform. That reduces validation effort from weeks to days, because the starting point reflects real-world lab workflows, not generic labware assumptions.
7. Service & Support Depth: From Firmware Updates to On-Site Calibration
A tester is only as reliable as its long-term support path. Ask: Does firmware update require sending the unit back? Are calibration certificates issued with uncertainty budgets matching your lab’s metrology hierarchy? Can field engineers diagnose sensor drift remotely—or do they need physical access to replace a load cell? For labs operating across APAC, EMEA, and North America, regional service coverage matters more than global headquarters claims. Paratronix Instruments Co., Ltd. commits to R&D and sales of packaging testing instruments alongside comprehensive, localized technical support—not just spare parts logistics. That means firmware patches address region-specific regulatory updates (e.g., PMDA guidance on needle sharpness reporting), and service engineers understand local calibration lab requirements before arriving onsite.
Selecting a syringe needle tester isn’t about checking boxes against ISO 7886—it’s about ensuring every test result stands up to scrutiny during internal audits, regulatory inspections, or supplier qualification reviews. Each of these seven parameters interacts: inaccurate force measurement undermines deflection repeatability; poor fixture design invalidates speed control; weak software validation erodes data integrity regardless of hardware precision. The most capable systems treat them as interdependent layers—not isolated specs.
If your current process relies on manual force gauges or legacy testers lacking full ISO 7886-1:2017 coverage, start by mapping which parameter gaps pose the highest risk—not just for compliance, but for detecting meaningful shifts in needle performance across suppliers or production runs. Then evaluate vendors not on brochure claims, but on how transparently they document trade-offs: Where does their stated accuracy hold? Under what environmental conditions? With which needle types? And how much of the validation burden remains yours versus theirs?
For labs needing integrated solutions across pharmaceutical packaging, plastic packaging material, and high barrier material testing, Paratronix Instruments Co., Ltd. develops instruments grounded in daily lab reality—not just standard clauses. Their approach reflects a commitment to research, development, and delivery of packaging testing instruments that serve as working tools—not compliance artifacts.
Leave A Reply
Search by Keywords