




Recent Posts
 Does your paper thickness tester meet ISO 534 requirements?Nov 17, 2026
 How does a laboratory bottle wall thickness tester work?Nov 16, 2026
 What Does a Beverage Bottle Wall Thickness Tester Measure?Nov 16, 2026
 What Does a Wall Thickness Tester Check in Cosmetic Bottles?Nov 16, 2026
 Can an ASTM E96 WVTR tester measure coated paper?Nov 14, 2026
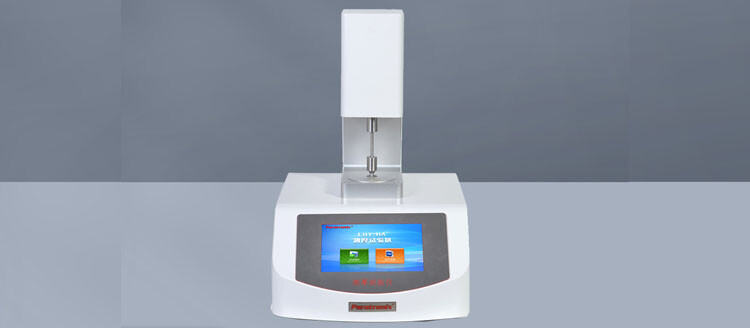
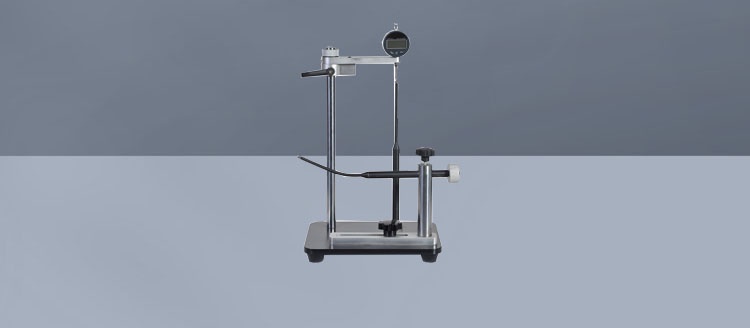
A paper thickness tester meets ISO 534 requirements only when its measuring geometry, applied pressure, indication and operating procedure conform to the applicable edition of the standard. A fine display resolution or a calibration certificate alone does not establish conformity. The test result also depends on specimen preparation, conditioning and the way the measuring surfaces contact the paper.
Begin by identifying the ISO 534 edition specified in the relevant material specification or test agreement. Then compare the instrument’s documented characteristics and the actual test procedure with that edition. A claim that a tester is “suitable for paper” is useful background, but it does not answer whether the complete measurement system satisfies the method.
Start with the measurement being reported
ISO 534 addresses the determination of thickness, density and specific volume of paper and board. These properties are related, but they are not interchangeable. Thickness is a distance measured under defined contact conditions. Apparent bulk density is calculated from grammage and thickness; specific volume is the reciprocal expression of density when consistent units are used.
The distinction matters when comparing reports. A thickness value obtained from an individual sheet does not necessarily agree with a value derived from a stack. Under compression, adjacent sheets and air spaces behave differently from a single sheet between measuring surfaces. The applicable standard and material specification determine which measurement and calculation are appropriate. Record the method alongside the result rather than labeling every value simply “caliper.”
For example, a change in calculated density can arise even when grammage remains stable: a lower measured thickness produces a higher calculated density. Before treating that change as a production shift, establish whether the test pressure, contact surfaces, conditioning and measurement method were consistent.
The measuring head determines more than resolution
A compliant paper thickness tester needs measuring surfaces of the geometry and dimensions required by the specified edition of ISO 534. The contact faces must also meet its requirements for condition and alignment. A small defect, contamination or lack of parallelism can concentrate contact on part of the specimen and change the compression under the measuring head.
Examine the anvil and pressure foot as a pair. A clean-looking surface can still have a burr, wear mark or residue that affects contact. A zero reading taken with the faces closed is useful, but it cannot by itself demonstrate that the faces are parallel across the contact area or that their dimensions are correct. Evidence of those characteristics should come from the instrument documentation and suitable inspection or verification.
Measuring pressure must be assessed together with the contact area. Pressure is the applied force divided by the area over which it acts. A force measurement alone is therefore insufficient if the pressure-foot area is wrong or damaged. Equally, a correctly sized foot does not establish the correct pressure if the applied force is outside the standard’s tolerance.
Paper is compressible, so excess pressure tends to reduce the indicated thickness. The effect is particularly relevant when comparing soft, textured or bulky material with a dense, smooth sheet. A tester that agrees well on a rigid reference may still produce biased paper results if its force or contact conditions are unsuitable.
Movement and contact need attention too
The way the pressure foot approaches the specimen affects the load applied at contact. Dropping the foot onto a sheet, holding it down by hand or allowing a mechanism to stick can produce a different reading from controlled, repeatable contact. Compare the instrument’s operation with the standard’s requirements for applying the measuring pressure and taking the reading.
If the display continues to change after contact, investigate the cause before selecting a reading. Possible explanations include gradual compression of the material, mechanical friction or instability in the indication. Consistent timing matters when the material responds to sustained loading; the specified method, rather than an arbitrary waiting period, should govern when the result is taken.
Calibration is necessary, but it answers a narrower question
Calibration evidence should cover the characteristics relevant to the measurement, including the indication over the intended measuring range. It should identify the instrument, the points tested, the results and the traceability of the reference standards. Review the reported errors and uncertainty against the tolerances and decision rules applicable to the work.
A certificate showing agreement with reference thickness standards does not automatically verify pressure, contact geometry, parallelism or the prescribed movement of the measuring head. Those characteristics need their own evidence where required. Conversely, an instrument with correct mechanical geometry still needs an indication that performs adequately across the thickness range being measured.
Resolution and accuracy also answer different questions. A display with many decimal places shows small increments; it does not prove that those increments represent the true displacement. For thin samples, zero error and repeatability can be significant relative to the reported thickness. For thicker board, performance near the upper part of the working range deserves attention as well.
Routine verification between calibrations can reveal drift or damage early. Use suitable reference standards, keep their contact faces clean, and record the readings under a consistent procedure. A reference outside the expected range, or a sudden change from earlier readings, calls for investigation before affected material results are accepted. Repeating a zero adjustment until a reference appears acceptable can conceal an underlying fault.
Conditioning and specimen selection affect the answer
Paper exchanges moisture with its surroundings, and moisture affects its dimensions and mechanical response. Specimens should be conditioned and tested under the atmosphere required by the applicable procedure. Record the conditioning conditions and any permitted departure from them. Testing a sheet immediately after it arrives from a different environment can produce a result that is difficult to compare with an earlier conditioned measurement.
Choose specimens according to the sampling and preparation rules that apply to the material. Keep the measuring area free from folds, creases and visible damage unless those features are part of the defined test. Do not press, rub or handle the intended measuring spot unnecessarily: local compression or contamination can change the contact response.
Surface variation deserves particular care. A textured sheet may give different readings at different locations because the pressure foot contacts high points and compresses the structure beneath them. Taking repeated readings at the same spot answers a repeatability question at that location; measurements at distinct locations also reveal material variation. The specified number and distribution of measurements should be followed when calculating the reported result.
For board with pronounced unevenness, a single value may conceal a wide spread across the specimen. Retaining individual readings as well as the required reported value helps distinguish a locally irregular sample from an instrument problem. If results are unexpectedly scattered, inspect both the sheet and the measuring faces before changing the acceptance decision.
When two testers disagree
Start with the reported method and specimen history. Confirm whether both results represent single-sheet thickness or a stack-based measurement, whether the samples came from comparable locations, and whether they experienced equivalent conditioning. A disagreement between different specimen types is not evidence of an instrument fault.
If the comparison is still meaningful, use the same prepared material and a documented sequence of measurements. Compare the instruments’ contact geometry, applied pressure, zero stability and calibration evidence. Also examine how the foot is lowered and when each reading is recorded. For compressible material, differences in pressure or contact time can produce a consistent offset even when both displays agree with a rigid reference.
A varying offset suggests a different investigation. Dirt on a contact face, a damaged specimen area, inconsistent positioning or a sticking mechanism can cause intermittent changes. Repeated measurements on a reference and on several locations of the sheet help separate instrument instability from local paper variation. Avoid using a correction factor to force agreement until the cause is understood and the permitted reporting procedure is established.
Density calculations need matched inputs
When apparent bulk density is required, pair thickness with the corresponding grammage using the calculation and units specified by the method. Grammage is mass per unit area; thickness is a distance. Unit conversion is essential because a numerically plausible result can still be wrong by a large factor if the thickness unit is misread.
Use the appropriate thickness result for the density quantity being reported, and keep the grammage and thickness measurements linked to representative material. Combining a current thickness result with an unrelated historical grammage value weakens the calculation. Likewise, a density calculated from stack thickness should not be compared without qualification with one calculated from individual-sheet thickness.
Thickness uncertainty carries into the density result. When a measurement sits close to a specification limit, consider the measurement uncertainty and the agreed decision rule before assigning a pass or fail. Rounding the thickness too early can also alter the calculated value; retain sufficient precision through the calculation and round the final report according to the applicable instructions.
What the test record should make traceable
A useful report identifies the material, the standard and edition applied, the measurement type, the conditioning and test conditions, and the result in the required units. Include the number of measurements and any departures from the method where relevant. If density or specific volume is reported, retain the input values and calculation basis so the result can be reconstructed.
The instrument record should connect the result to a specific tester and its verification status. If a reference check later reveals a problem, that link makes it possible to identify the measurements that need review. It also prevents a replacement instrument, a changed pressure foot or a revised procedure from silently becoming part of a historical comparison.
Conformity is a documented relationship between the specified method, the equipment’s verified characteristics and the conditions under which the test was performed. Where the available evidence does not cover one of those elements, the result may still be useful for an internal comparison, but a claim of conformity to ISO 534 remains unsubstantiated until the gap is resolved.
Leave A Reply
Search by Keywords