

Recent Posts
 How test speed affects lipstick breaking strength resultsOct 10, 2026
 Choosing a Water Vapor Transmission Rate Tester for flexible filmsOct 10, 2026
 How to select a friction peel tester for flexible packaging filmsOct 09, 2026
 Key Specifications to Compare When Selecting a Lipstick Break Force TesterOct 08, 2026
 What Does a Lipstick Break Force Tester Measure in Quality Control?Oct 08, 2026
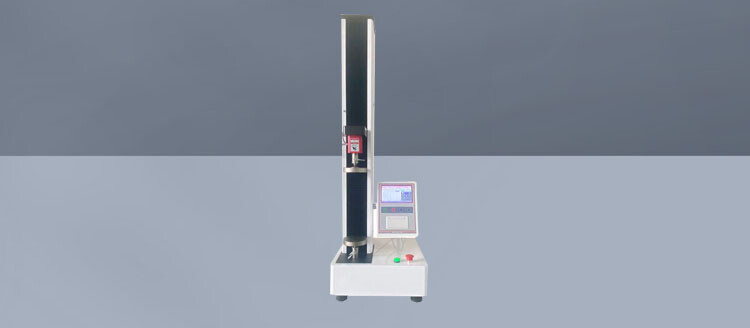
A lipstick can appear firm during routine inspection yet fracture unexpectedly when it is extended, pressed against the lips, or exposed to a minor side load. When this happens, the test result is often questioned first: was the formula weak, was the stick improperly conditioned, or did the test method create a misleading force value? In many cases, the answer lies in test speed.
Test speed directly affects lipstick breaking strength results because lipstick is a rate-sensitive, viscoelastic product. A faster loading speed can produce a higher apparent breaking force, while a slower speed may allow the wax-and-oil structure to deform, relax, or crack at a lower force. Neither result is automatically “correct” on its own. The useful result is the one obtained at a defined speed that reflects the intended handling condition and can be repeated reliably.
Why a change in speed changes the measured force
A lipstick bullet is not a rigid plastic part. Its mechanical response is governed by a structure of waxes, oils, pigments, powders, polymers, and other ingredients. Temperature, crystal arrangement, aging, and solvent migration can all alter that structure. When force is applied, the material may show elastic recovery, permanent deformation, creep, or brittle cracking, often in combination.
At a slow test speed, stress has more time to redistribute through the lipstick matrix. The material may bend gradually, show visible yielding near the base, or develop a crack after substantial deflection. Some internal resistance relaxes during loading, so the maximum recorded force can be relatively low. This condition can reveal softness, poor structural cohesion, or insufficient support from the formula.
At a high test speed, the applied stress rises more quickly than the material can relax. The lipstick may behave as though it is stiffer, producing a higher peak load before failure. It may also fracture more suddenly, with less visible bending. This does not necessarily mean the product has become stronger in practical use; it may simply be responding differently because the loading rate changed.
The relationship is particularly important when comparing batches. A difference in breaking force may appear to indicate a formulation issue, but a changed crosshead speed, a different manual operating rhythm, or inconsistent trigger settings can create a similar shift. A lipstick breaking strength tester removes much of the operator-related variation, but the programmed test speed still needs to be controlled as part of the method.
Apparent strength is not always product strength
Breaking strength is commonly reported as the maximum force reached before a fracture event, a rapid load drop, or a specified deformation limit. That value is useful, but it is not a universal material constant. It is a result generated under a particular combination of sample geometry, support condition, temperature, probe position, loading direction, and speed.
Consider two tests on visually identical bullets. In the first test, the probe advances slowly and the bullet bends for a noticeable distance before cracking. In the second, the probe moves faster and the bullet breaks with a sharp force peak. The second result may show a larger maximum force even though the product is more prone to sudden fracture during certain types of use. Looking only at the peak value can therefore hide an important difference in failure behavior.
For quality decisions, it is often helpful to observe more than one result feature:
- Peak force: the highest resistance recorded before failure or the end of the test.
- Displacement at peak force: how far the bullet moved or bent before reaching its maximum load.
- Failure mode: clean snap, partial crack, bending, crushing, detachment from the cup, or no failure within the travel limit.
- Shape of the force-displacement curve: a gradual rise, plateau, sudden drop, or multiple drops can indicate different structural behavior.
A batch that meets a minimum force requirement at one speed may still deserve review if it shows unusually low displacement before breakage or an abrupt failure pattern compared with established control samples. This is especially relevant where the product must tolerate incidental side loading after extension from its package.
The speed effect depends on the test arrangement
Test speed cannot be selected separately from the fixture and loading geometry. Lipstick breaking evaluation is often performed by holding the lipstick in its package or sample holder, extending the bullet to a defined height, and applying force at a defined point from the side. This creates a bending load. Small variations in exposed length or probe location can strongly change the bending moment, so they must not be mistaken for a speed effect.
When the load is applied farther from the base of the bullet, the leverage increases and lower force may be required to cause failure. When the bullet is extended higher, it is more vulnerable to bending. A test method that changes both extension height and speed cannot identify which variable caused the result shift.
The probe itself matters as well. A narrow contact tip concentrates stress and may initiate cracking at lower force than a broader contact surface. A rough, contaminated, or misaligned probe can drag the lipstick surface rather than apply a clean perpendicular load. Before comparing speeds, confirm that the contact shape, approach direction, and contact position are unchanged.
When fast testing creates misleading confidence
Faster testing is sometimes chosen to improve throughput. That can be reasonable when the method has been validated at that speed and the loading condition represents the intended product risk. Problems arise when a faster setting is adopted only because it shortens the test cycle.
A quick test can make a soft or relaxation-prone formula look stronger than it behaves during slow application pressure. It can also reduce the time available to see progressive deformation, base instability, or partial separation between the bullet and its holder. A sharp peak may look favorable in a spreadsheet while masking a brittle failure mode that is undesirable in use.
Fast testing may also increase the influence of instrument dynamics. If the frame, fixture, or sample holder has small amounts of compliance, rapid loading can introduce oscillation or a transient force overshoot. A tester with an appropriate load sensor, controlled drive, adequate data acquisition rate, and stable fixture design helps reduce these effects. Still, equipment capability does not eliminate the need to use a sensible and documented speed.
Where rapid loading is relevant, such as assessing accidental impact-like handling, it is better to describe the test as a distinct condition rather than treating it as interchangeable with a standard bending-strength measurement. Results from the two conditions may both be useful, but they answer different questions.
What slow testing can reveal—and what it can distort
Slower movement is often useful when the goal is to understand deformation before fracture. It can show whether the bullet yields at the base, creeps under load, or remains intact but permanently bent. This type of response may be important for products that are exposed to sustained application pressure or remain extended for a period during use.
However, extremely slow testing can introduce its own complications. The sample may experience time-dependent creep rather than a practical break event. Surface warming from the environment, changes in exposed sample condition, or gradual slippage in the holder may become more influential. If a test takes too long, the result may represent prolonged static loading rather than ordinary use.
Slow loading also requires an unambiguous endpoint. A lipstick may not produce a dramatic force drop when it yields or partially cracks. The method should state whether the result is the maximum force, force at a specified displacement, force at a defined deformation angle, or force at the first confirmed fracture. Without a clear endpoint, two operators may interpret the same curve differently.
Choosing a speed for a controlled method
There is no single speed that suits every lipstick formula, bullet geometry, or quality objective. The most defensible approach is to establish a speed through method development, then retain it for routine comparison. The chosen condition should be slow enough to avoid unnecessary dynamic artifacts and fast enough to provide a practical, repeatable test with a clearly identifiable failure response.
Start by defining the real question behind the measurement. A release test may need a stable batch-to-batch indicator. A formulation development test may need greater sensitivity to structure changes. A complaint investigation may need to reproduce a specific handling condition, such as breakage during use after full extension. Those purposes may justify different test conditions, but each condition should be documented as a separate method.
Use a small speed study before locking the method
Test comparable, properly conditioned samples at several deliberately selected speeds within the operating range of the equipment. Keep every other condition fixed: sample temperature, time after manufacture where relevant, extension height, probe position, fixture, load cell, preload or contact detection setting, and endpoint rule.
Do not select a speed solely because it produces the highest force or the lowest variation in a limited set of samples. Review whether the failure mode remains consistent. A speed is more useful when the force-displacement curves are stable, the observed failure corresponds to the intended product risk, and small changes in operator handling do not alter the setup.
During the study, record:
- the programmed crosshead or probe speed;
- the actual sample extension height from the support point;
- the loading location and direction;
- the conditioning temperature and duration;
- peak force and displacement at peak force;
- the visual failure description, including whether failure occurred at the bullet base, mid-section, or cup interface.
These records make later troubleshooting far easier. When a result changes, the team can determine whether the cause is material behavior, sample preparation, or a change in test execution.
Temperature can magnify the influence of speed
Temperature and speed should be considered together. A lipstick tested at a warmer temperature generally becomes softer and more able to deform. Under slow loading, that softening may be especially visible because the structure has time to flow or relax. Under faster loading, the same warm sample may still show a temporary increase in apparent stiffness compared with its slow-speed result, but its failure pattern can remain very different from that of a properly conditioned sample.
Testing samples before they reach a consistent temperature is a frequent source of confusing data. A bullet removed from a cold storage area may seem unusually strong at first, while a recently warmed sample may bend or detach at a lower force. Changing speed to compensate for these differences is not a valid correction. Control the conditioning environment first, then evaluate speed effects under that controlled condition.
When results appear inconsistent only during certain times of day or after a change in storage practice, review sample temperature records before adjusting acceptance limits. A stable speed cannot compensate for uncontrolled thermal history.
Signs that the current speed needs review
A method review is justified when the test no longer produces a clear or useful distinction between acceptable and questionable samples. Several observations can indicate that speed is part of the issue:
- Replicate force values vary widely even though samples look similar and were conditioned together.
- The curve shows a brief spike that is not supported by visible sample resistance or a meaningful fracture event.
- Most samples reach the travel limit without failure, making peak force difficult to interpret.
- Samples show different failure modes at the same nominal force level.
- A formulation change appears to improve strength only under a faster test condition.
- Results differ substantially after an instrument, fixture, or operator change despite unchanged product specifications.
Before changing the speed, verify basic mechanical controls: fixture alignment, exposed bullet length, probe cleanliness, load sensor range, zeroing, contact detection, and data sampling settings. A speed adjustment made to solve a fixture or setup problem can reduce repeatability rather than improve it.
Writing the speed into the test instruction
A workable instruction should state more than “test breaking strength.” It should identify the test speed in the same units used by the instrument, along with an allowed tolerance if the internal quality system uses one. It should also define whether speed refers to the initial approach, the loading movement after contact, or the entire test cycle. On some systems, approach speed and test speed can be configured separately; confusing the two can create inconsistent contact conditions.
Include the stop condition and data rule. For example, the method may stop after a confirmed force drop, after a defined travel distance, or when a specified force is reached. It should state how to treat a sample that bends but does not break, a sample that slips from the holder, or a bullet that separates from its cup rather than fracturing. These are not merely operator notes; they determine whether results remain comparable over time.
A lipstick breaking strength tester is most valuable when it converts a subjective handling concern into controlled mechanical evidence. Keeping test speed fixed, selecting it for the intended loading condition, and reviewing force together with deformation and failure mode will produce results that are more repeatable and more useful for quality and safety decisions.
Leave A Reply
Search by Keywords