

Recent Posts
 Which standards should an ampoule break force tester support?Sep 20, 2026
 Using a Leakage Tester to Meet ISO 11607 Package Integrity RequirementsSep 20, 2026
 Using Leak and Seal Strength Tests for Medical Pouches and Sterile Barrier SystemsSep 18, 2026
 How Leak and Seal Strength Testers Use Vacuum Decay, Burst, and Peel MethodsSep 18, 2026
 Which Features Have the Greatest Impact on Puncture Force Tester Cost?Sep 17, 2026
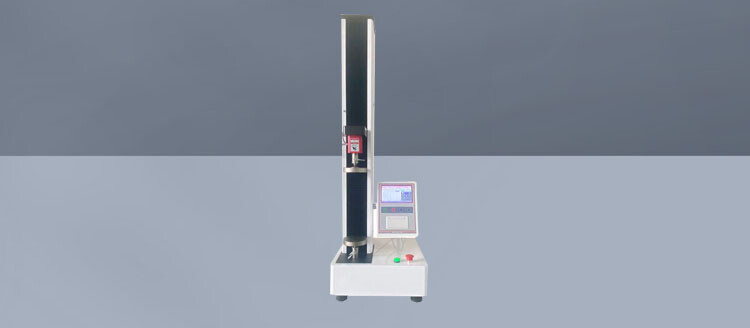
Which Standards Should an Ampoule Break Force Tester Support?
Selecting an ampoule break force tester is essential for quality and safety teams seeking consistent ampoule opening performance, patient safety, and reliable packaging compliance.
The right instrument should support relevant pharmacopeial and international testing standards while delivering accurate force measurement, repeatable results, and flexible test configurations.
This guide explains the key standards and capabilities to consider when evaluating ampoule break force testing equipment for pharmaceutical packaging quality control operations.
Start with the Real Quality and Safety Requirement
Quality teams do not purchase an ampoule break force tester simply to obtain a numerical force value for a laboratory report.
They need evidence that an ampoule opens predictably, without excessive effort, dangerous glass fragmentation, or unacceptable variation between production batches.
Break force directly affects the daily experience of healthcare professionals who must open sterile injectable products under controlled clinical conditions.
If the required opening force is too high, users may apply unstable or excessive force, increasing the risk of hand injury.
If the force is too low, the ampoule may break unintentionally during handling, transport, labeling, secondary packaging, or dispensing operations.
For safety managers, the critical question is whether the tester can identify ampoules that create practical opening hazards before products reach users.
For quality control personnel, the priority is whether results are repeatable, traceable, and suitable for batch release, investigation, and supplier qualification.
Therefore, the best ampoule break force tester should support recognized standards while also allowing the company to manage product-specific acceptance limits.
ISO 9187-1 Is the Primary Standard to Assess
For glass ampoules intended for injectable preparations, ISO 9187-1 is generally the most important international reference for break force testing.
ISO 9187-1 covers one-point-cut ampoules and defines requirements related to dimensions, material performance, opening behavior, and test procedures.
The standard is especially relevant when evaluating ampoules with a color break ring, ceramic break point, or other intentional opening feature.
Its break force method provides a structured basis for measuring the force required to separate the ampoule head from the body.
An ampoule break force tester should be able to perform the prescribed loading arrangement and maintain the appropriate alignment during testing.
Misalignment can introduce bending, twisting, or uneven loading, producing readings that do not accurately represent real ampoule opening behavior.
Ask the instrument supplier whether the fixture design is specifically intended to support the ISO 9187-1 test principle, rather than generic compression testing.
A universal tensile or compression tester may measure force, but it may not provide the correct ampoule support geometry or controlled breaking position.
The tester should also accommodate the ampoule formats used in your facility, including different diameters, neck dimensions, and fill-volume configurations.
Understand the Relevance of ISO 9187-2
ISO 9187-2 is another relevant standard because it addresses one-point-cut ampoules and their performance within pharmaceutical packaging applications.
Quality teams should review both ISO 9187-1 and ISO 9187-2 when defining internal specifications for ampoule design and opening performance.
These standards help manufacturers establish common terminology, dimensional expectations, and testing logic across pharmaceutical companies, converters, and glass ampoule suppliers.
However, standards should not be treated as a substitute for a documented product-specific risk assessment and validated internal quality control procedure.
A specific ampoule design may require narrower force limits because of its neck geometry, glass composition, filling line conditions, or intended clinical environment.
For example, a small ampoule used frequently in hospital wards may require a different opening-force target from a larger specialty injectable product.
The tester should therefore allow laboratories to create controlled test methods that reflect both external standards and approved internal specifications.
Flexible method management reduces the risk of relying on manual adjustments, handwritten records, or undocumented changes between operators and production sites.
Check Applicable Pharmacopeial Expectations
Pharmacopeial requirements often focus on material suitability, container quality, extractables, particulate control, and product protection rather than one universal break-force limit.
Nevertheless, pharmacopeial expectations remain important because ampoule opening performance is closely connected with patient safety and packaging quality risk management.
European Pharmacopoeia requirements for glass containers used for pharmaceutical products can influence material selection, quality documentation, and supplier control activities.
USP chapters concerning packaging systems and glass containers may also inform the broader compliance framework for injectable drug product manufacturers.
When reviewing an ampoule break force tester, confirm that its data output can support your pharmaceutical quality system and regulatory documentation practices.
The instrument should retain test conditions, measured values, sample identifiers, operator details, calibration status, and pass-fail conclusions where required.
For regulated facilities, a force result without traceable context may have limited value during audits, deviations, complaint investigations, or product quality reviews.
Quality assurance should determine whether electronic records need to comply with data integrity controls, including user access, audit trails, and electronic signatures.
Do Not Assume There Is One Universal Force Limit
One of the most common mistakes in ampoule testing is searching for a single opening-force requirement that applies to every glass ampoule.
In practice, acceptable break force depends on ampoule size, neck diameter, score design, glass thickness, manufacturing process, and intended product use.
ISO-based methods provide the measurement framework, while acceptance criteria are often defined through applicable standards, customer agreements, validation, and risk assessment.
Quality teams should establish both lower and upper force limits instead of only rejecting ampoules that require excessive opening force.
An unusually low force result may indicate weak score formation, inconsistent annealing, neck defects, or poor resistance to handling stresses.
An unusually high force result may indicate an incomplete score, poor score positioning, excessive glass thickness, or variation in production tooling.
Trend analysis is often more informative than individual results because gradual changes can reveal developing process problems before product failure occurs.
The ampoule break force tester should support statistical analysis such as average values, standard deviation, maximum values, minimum values, and distribution review.
Fixture Design Matters as Much as Load Cell Accuracy
Load cell accuracy is essential, but it does not guarantee reliable break-force testing when the ampoule fixture cannot hold samples consistently.
The fixture should secure the ampoule body while applying force to the ampoule head at the intended location and direction.
It should prevent sample rotation without creating localized stress points that alter the natural breaking behavior of the glass neck.
Adjustable supports are valuable when a quality control laboratory tests multiple ampoule formats, including different nominal volumes and neck diameters.
However, frequent manual fixture changes can introduce variability unless positions are easy to reproduce and documented within approved test methods.
Ask whether the fixture includes defined locating surfaces, scale markings, change parts, or guided adjustment mechanisms for repeatable sample positioning.
The instrument should also protect operators from sharp fragments during testing through guards, shields, enclosed test areas, or appropriate safety accessories.
Because ampoule fracture is intentional, safety features should be evaluated as functional laboratory controls rather than optional cosmetic additions.
Force Range, Resolution, and Sampling Rate Need Review
An ampoule break force tester must use a force range suitable for expected ampoule opening values while retaining adequate measurement resolution.
Choosing an excessively large load cell can reduce sensitivity and make small but meaningful differences between samples more difficult to identify.
Conversely, choosing an undersized load cell may create overload risks or restrict the tester’s usefulness for larger or stronger ampoule designs.
Discuss the anticipated test range with the equipment supplier and select a load cell that provides practical measurement capability within that range.
Resolution should be sufficient to distinguish routine process variation from meaningful changes that may require corrective action or additional sample investigation.
Sampling rate also matters because glass fracture can occur rapidly, producing a peak force that slow data acquisition may fail to capture accurately.
The system should record the maximum break force and ideally display the complete force-versus-displacement curve for technical evaluation.
Curve review can help investigators distinguish normal fracture behavior from slippage, fixture interference, sample misalignment, or abnormal multi-stage breakage.
Test Speed and Method Control Affect Comparability
Break force results can change when the loading speed changes, particularly for fragile glass structures and differently designed break points.
For this reason, an ampoule break force tester should provide controlled, repeatable test speed settings consistent with the selected test method.
Operators should not need to apply manual force because manual testing introduces uncontrolled speed, angle, grip variation, and subjective judgment.
Motorized testing improves repeatability by applying force in a programmed manner and reducing dependence on individual operator technique.
The tester should allow laboratories to save test speed, return position, force threshold, sample quantity, and result calculation settings in named methods.
Method protection is especially useful in multi-shift operations where different operators, supervisors, and sites must follow the same approved procedure.
Controlled methods also simplify training because laboratory staff can select a validated procedure instead of entering critical parameters each time.
This reduces the likelihood that a reporting difference is caused by setup inconsistency rather than an actual change in ampoule quality.
Data Integrity and Traceability Are Essential in Regulated Operations
For pharmaceutical packaging quality control, reliable mechanical testing must be supported by reliable records and controlled data management practices.
A basic display-only tester may be adequate for development work, but it can create avoidable administrative risk in GMP manufacturing environments.
Consider whether the ampoule break force tester provides result storage, electronic report generation, user permissions, audit trails, and secure data export.
These features are particularly valuable when test data support batch disposition, supplier performance reviews, process validation, or deviation investigations.
Audit trail capability should document changes to test methods, specifications, user settings, and reported results in a reviewable form.
User roles should prevent unauthorized personnel from changing acceptance criteria or calibration-related settings without appropriate quality authorization.
Reports should identify the sample, batch, date, test method, instrument, operator, force results, and pass-fail determination clearly.
When software is involved, quality teams should assess whether the supplier can provide documentation supporting computer system validation and data integrity review.
Calibration and Measurement Traceability Must Be Practical
Even a well-designed ampoule break force tester cannot provide defensible results if its force measurement system is not properly calibrated and maintained.
The equipment should support calibration using traceable reference standards appropriate for the operating range and required measurement uncertainty.
Laboratories should define calibration intervals based on risk, usage frequency, manufacturer guidance, quality procedures, and historical performance evidence.
Before routine testing, operators may also need to perform verification checks to confirm that the instrument remains suitable for use.
Verification procedures should be practical enough to complete consistently without creating excessive laboratory workload or undocumented workarounds.
Ask whether the supplier provides calibration support, service procedures, spare parts availability, and clear guidance for routine performance confirmation.
For organizations operating under ISO 17025 principles, calibration records and uncertainty considerations should be aligned with the laboratory’s overall quality system.
Traceability is not merely an audit requirement; it determines whether a borderline force result can be trusted when a release decision is required.
Use Risk-Based Sampling and Trending Rather Than Isolated Results
Ampoule break force testing provides the greatest value when it is integrated into a broader packaging quality control and process-monitoring strategy.
Testing only one sample after a line adjustment may not reveal variability caused by tool wear, glass lot differences, or scoring instability.
Sampling plans should consider production volume, supplier history, process capability, product criticality, and the potential consequences of opening failures.
Incoming inspection may require different sampling rules from in-process control, validation studies, complaint investigations, or periodic supplier requalification activities.
Quality teams should review force trends by cavity, machine, mold set, production shift, glass supplier, ampoule format, and product family.
Such analysis can identify recurring patterns that may remain hidden when results are reviewed only as individual pass-fail decisions.
When results approach control limits, investigate related indicators such as visual score quality, dimensional variation, annealing conditions, and breakage complaints.
An ampoule break force tester with exportable raw data makes this type of analysis faster and more reliable than manually transcribed results.
Questions to Ask Before Selecting an Instrument
Before purchasing, ask which ampoule standards and methods the tester supports through its fixture design, software configuration, and documented operating procedures.
Request sample testing using your own ampoule formats, especially where the product includes unusual neck designs or difficult-to-open glass structures.
Compare repeatability between multiple operators rather than relying only on a supplier demonstration performed by an experienced application specialist.
Ask how easily the tester can be adjusted for different ampoule sizes and whether changes require tools, replacement fixtures, or software modifications.
Review whether result records meet the needs of your quality system, including report format, data retention, approval workflows, and electronic controls.
Confirm the expected service response, calibration options, installation support, training scope, and availability of local technical assistance before final approval.
Finally, evaluate the tester as part of the complete testing workflow, including sample preparation, safe fracture disposal, review time, and documentation requirements.
Conclusion
An effective ampoule break force tester should support ISO 9187 testing principles while allowing controlled methods for product-specific specifications and risk-based quality decisions.
For quality control and safety teams, the most important capabilities are accurate force measurement, proper fixtures, controlled speed, repeatable positioning, and traceable records.
Compliance should be evaluated beyond a standards checklist, because a tester must also support practical laboratory workflows, operator safety, calibration, and meaningful trend analysis.
By selecting equipment that combines recognized test support with flexible method control, manufacturers can improve ampoule opening consistency, reduce safety risk, and strengthen packaging quality assurance.
Leave A Reply
Search by Keywords